Weld Creations provides precision TIG welding services to manufacturers across Los Angeles and Southern California. TIG (gas tungsten arc welding, or GTAW) is our core process, and we’re AWS D17.1 certified to the aerospace fusion welding standard. We weld stainless steel, aluminum, titanium and nickel alloys, from single prototypes to production runs, in Glendora in the San Gabriel Valley.
Why TIG
TIG welding uses a non-consumable tungsten electrode, a separate filler rod and an inert shielding gas, usually argon. The welder controls heat continuously with a foot pedal or torch control. That control is the whole point:
- Thin material without burn-through. Thin-wall tube and light-gauge sheet need precise heat, which is exactly where TIG outperforms other arc processes.
- Clean, spatter-free welds. There’s no flux and no spatter, so welds are ready for polishing, passivation or visible installation.
- Exotic and reactive metals. Titanium and nickel alloys demand clean shielding and low, controlled heat input, and TIG provides both.
- Full-penetration root passes. With a back purge, the inside of a tube or closed section comes out as clean as the outside, which is essential for sanitary work.
The trade-off is speed. TIG is slower than MIG, so we choose the process to fit the part.
| TIG (GTAW) | MIG (GMAW) | |
|---|---|---|
| Heat control | Very fine | Moderate |
| Best for | Thin material, stainless, aluminum, titanium, nickel alloys, visible or sanitary welds | Thicker carbon steel, structural parts, speed |
| Weld appearance | Clean, no spatter | Good, may need cleanup |
| Speed | Slower | Faster |
We run both, and we’ll tell you which one your part actually needs.
Metals we TIG weld
- Stainless steel. 304/304L, 316/316L and more, for sanitary, pharmaceutical, food and architectural parts.
- Aluminum. Welded on AC, where the cleaning action of the arc breaks up the surface oxide, for enclosures, frames, brackets and aerospace components.
- Titanium. Needs full shielding until the weld cools. Weld color is a direct indicator of contamination, so shielding is non-negotiable.
- Nickel alloys. Hastelloy and Inconel for corrosive and high-temperature service, welded with matched fillers and low heat input.
- Carbon and chromoly steel. For precision frames, fixtures and components.
AWS D17.1 certified
AWS D17.1 is the American Welding Society’s specification for fusion welding of aerospace hardware. It covers the discipline side of welding: procedures, welder qualification, inspection and acceptance criteria. We bring that same discipline to every job, whether it’s flying or not.
Precision parts and production runs
TIG welding is often the deciding step in a precision part. The machining is done, the tolerances are tight, and the welding must not undo them. We control distortion with fixturing, weld sequence and heat management, so parts stay flat and in position.
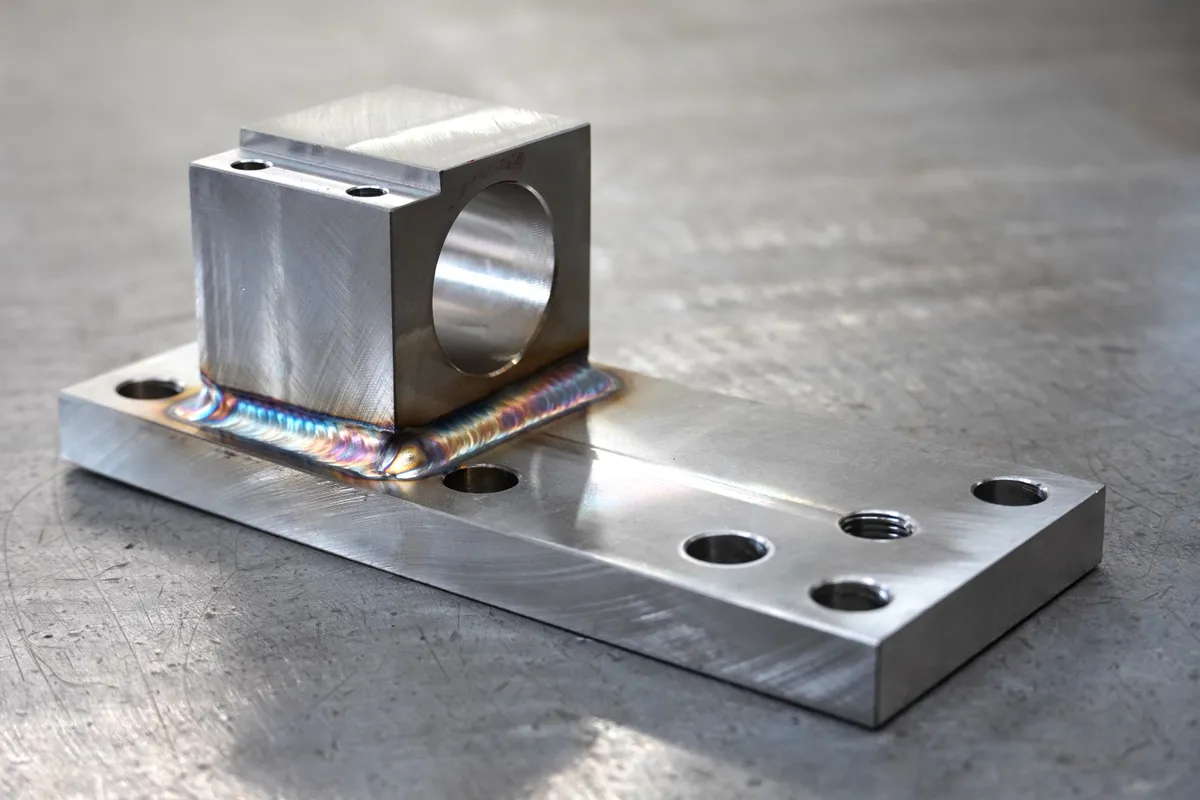
For repeat work, we build fixtures so every part matches the approved first article. The gallery shows one example: a run of identical stainless block-and-plate brackets, each with the same fillet profile. Read more about how we run production welding.
Welding on your parts
Much of our TIG work is welding components that customers supply: machined parts from a machine shop, formed sheet metal, or castings and assemblies that need a precise weld in the right place. When you send parts to us:
- Tell us the exact alloy (and temper, for aluminum), since filler selection depends on it.
- Mark critical dimensions and datums that must not move, so we can fixture around them.
- Call out weld size, finish and inspection requirements, such as a blended-flush weld on a visible surface or full penetration on a pressure boundary.
- Let us know about downstream processes like anodizing, passivation or machining after welding, because they affect filler choice and weld prep.
We return the parts welded, inspected and ready for the next operation.
Industries
- Pharmaceutical and nutraceutical. Cleanroom stainless, hoppers and machine frames. See pharmaceutical equipment fabrication.
- Food and beverage. Sanitary equipment and components.
- Aerospace. Precision welded components under AWS D17.1.
- Sheet metal and machining shops. Welding support for shops that need a trusted TIG partner.
Service area
We’re based at 2041 E Gladstone St in Glendora, with easy access to the 210 and 57 freeways. We serve manufacturers throughout Los Angeles County, Orange County and San Bernardino County, and we ship finished parts farther. For a printable overview for your purchasing team, see our capabilities.
Request a TIG welding quote
Send the drawing, material, quantity and timeline. For welding on parts you supply, tell us the alloy and any finish or inspection requirements. We reply within one business day.