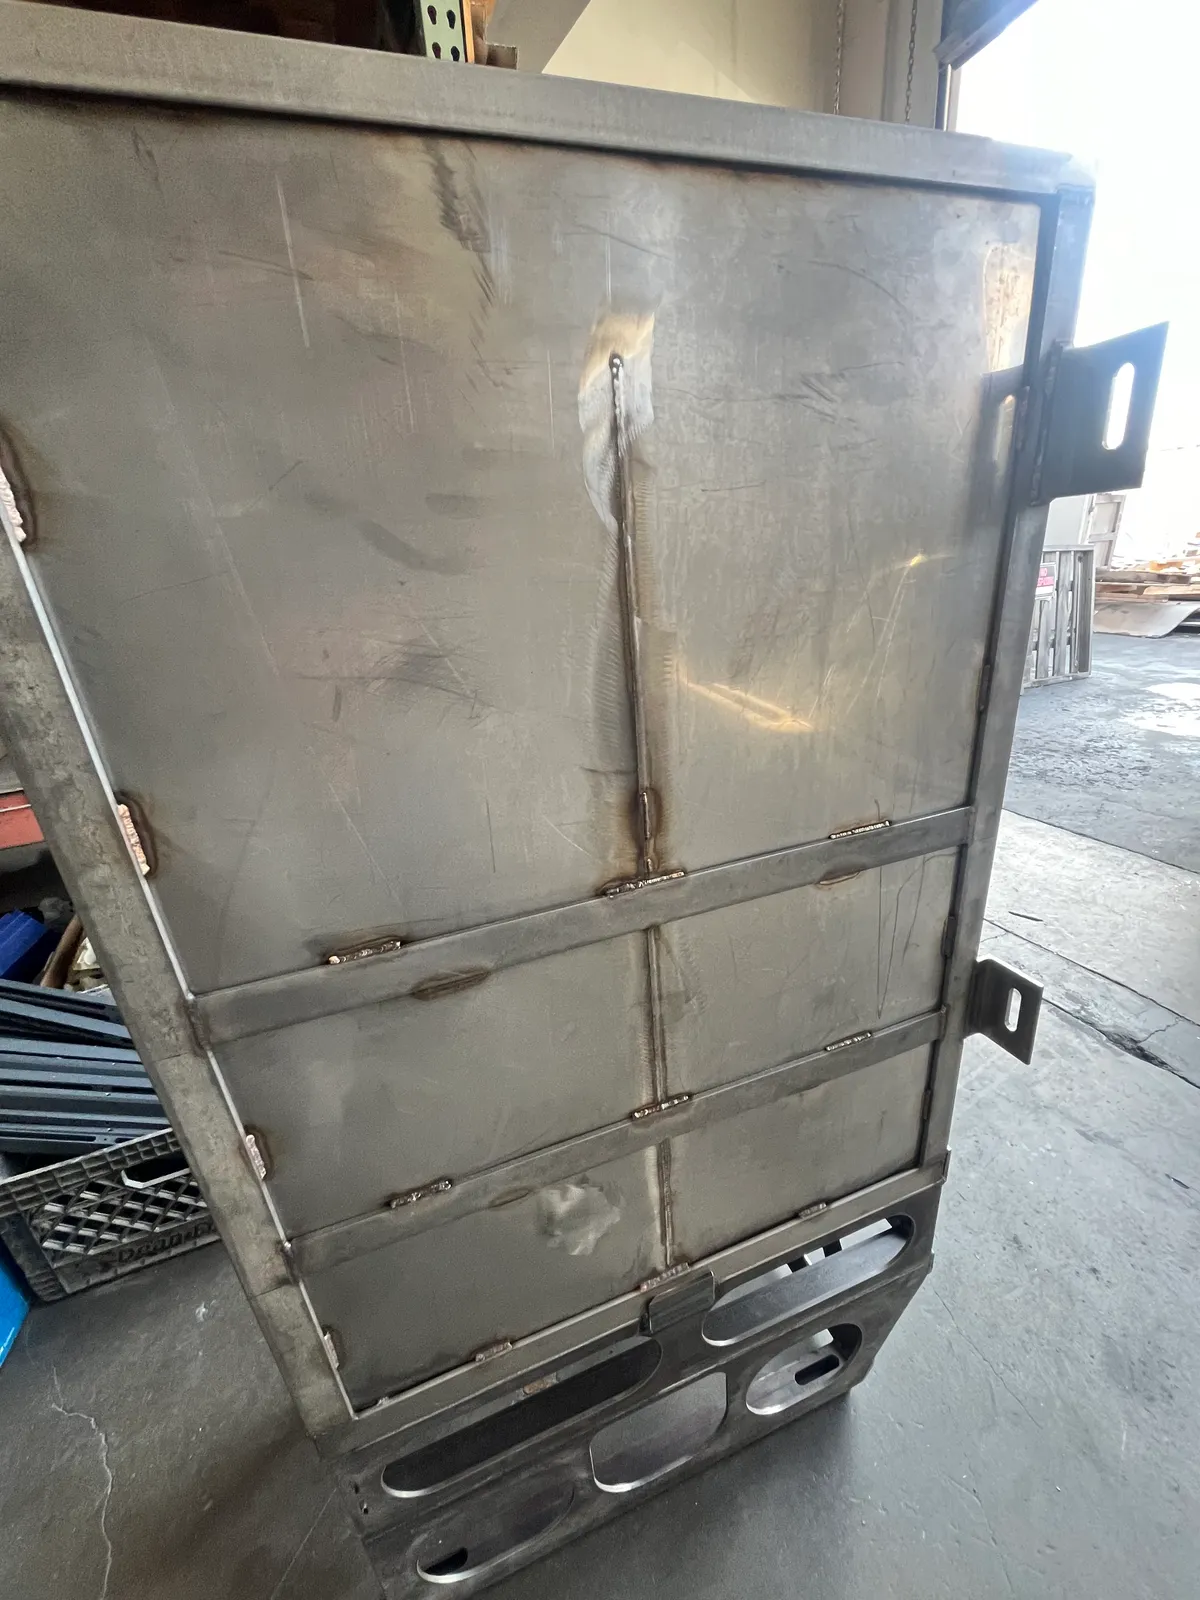
Weld Creations provides welding services for metal stamping companies: subcontract welding on your stampings, drawn shells and formed parts, built into finished assemblies and returned ready for your next operation. We run TIG, MIG and resistance spot welding under one roof, so a mixed assembly doesn’t have to be split between two suppliers. We’re AWS D17.1 certified, and the work stampers send us is the work that’s hard to keep in house, where thin material, a cosmetic weld or a certified joint puts a pressed part at risk.
Have stampings that need welding? Send the print and the quantity and we’ll quote per part. Request a quote.
Why stamping shops send welding out
A press floor is built around tonnage, dies and throughput. Welding doesn’t fit that rhythm, and it’s usually the operation that quietly holds up a shipment. Shops send it out when:
- The welder is the bottleneck. The presses are running and the weld cell is three weeks behind.
- The job is an assembly, not a part. Two or three stampings that have to become one component, with position and squareness that matter.
- The material is unforgiving. Thin-wall stainless, aluminum, titanium or a nickel alloy, where one burned-through weld scraps a part that already has tooling cost in it.
- The weld has to be certified. The print flows down a welding specification and there’s no certified welder on the floor.
- The weld will be seen. A part that gets polished, plated or powder coated shows every flaw in the weld underneath it.
- The die doesn’t exist yet. The customer needs samples now, and the production tool is eight weeks out.
We take that work as an extension of your shop, not as a competitor. You keep the customer, the program and the margin on the stamping.
What we weld for stampers
- Stampings into assemblies. Two or more pressed parts joined into a single component, fixtured so the critical dimension repeats.
- Deep drawn shells. Fittings, flanges, bosses and closures welded to drawn cups and housings, including leak-tight seam welds.
- Brackets, mounts and tabs welded to panels, plates and formed sections.
- Stampings welded to machined or tubular parts. Mixed assemblies where a pressed part meets a turned fitting, a tube or a machined block. See weldment fabrication.
- Closing and seam welds on formed housings, enclosures and covers.
- Spot welded lap joints and attachment. Resistance spot welding on sheet and stamped components, for assemblies where a fusion weld would put in more heat than the joint needs.
- Rework and salvage. Short-shipped runs, damaged parts and field returns, welded and blended rather than scrapped.
Thin gauge is the whole problem
Welding a stamping is not the same job as welding plate. The part is already formed to a dimension, it has residual stress from the press, and the material is often thin enough to burn through if the arc stops for a second too long. Our approach:
- Fixture first. Parts are located and clamped so they hold position through welding and cooling, not just while the torch is moving.
- Sequence the welds so heat is balanced around the part instead of pulling it one direction.
- Keep heat input low. TIG welding gives the finest heat control of any manual arc process. On gauge material that’s the difference between a part and a reject.
- Stitch where the design allows it, rather than running a continuous bead that distorts a panel.
- Prove it on a first article before the run, so you approve the real part and not a promise.
More on the technique in sheet metal welding.
Materials
Stainless steel in 304, 316 and the low-carbon L grades, aluminum in the 5xxx and 6xxx series, carbon, HSLA and chromoly steel, titanium, and nickel alloys including Hastelloy and Inconel. If you press an alloy that isn’t on this list, send the spec and we’ll tell you plainly whether we weld it, rather than finding out on your parts.
Prototype now, production later
A lot of stamping programs need parts before the die is finished. We weld soft-tooled, laser-cut and hand-formed components so you can ship samples, pass a customer trial or validate fit while the tool is being built. When the die lands and the part goes to volume, the same assembly moves to a fixture and a production run with per-part pricing.
Repeat work, priced per part
For recurring assemblies we build the fixture, weld and inspect a first article for your approval, and run against the approved part from then on. We quote per part, support blanket orders with scheduled releases, and hold the fixture here between releases so there’s no setup cost each time.
Documentation for your quality file
Tell us what your customer requires and we’ll deliver it alongside the parts: weld inspection results, dimensional reports, photographs, material and filler traceability, first-article documentation or a certificate of conformance. Our welding is certified to AWS D17.1, the aerospace fusion welding standard. If your program flows down a different approval, tell us up front and we’ll give you a straight answer about whether we can meet it.
Southern California and beyond
We’re in Glendora, about twenty-five miles from the Santa Fe Springs, City of Industry and Commerce stamping corridor, so local shops drop parts off and pick them up by appointment. Out-of-area stampers ship parts in and we ship them back, which works well for the welding operations that would otherwise sit in a queue. See Glendora welding or our capabilities.
What to send for a quote
The print or STEP file, the material and gauge, the quantity now and the expected annual volume, the weld requirements and any specification that applies, the features that must hold position, and what happens to the part after welding. We reply within one business day.